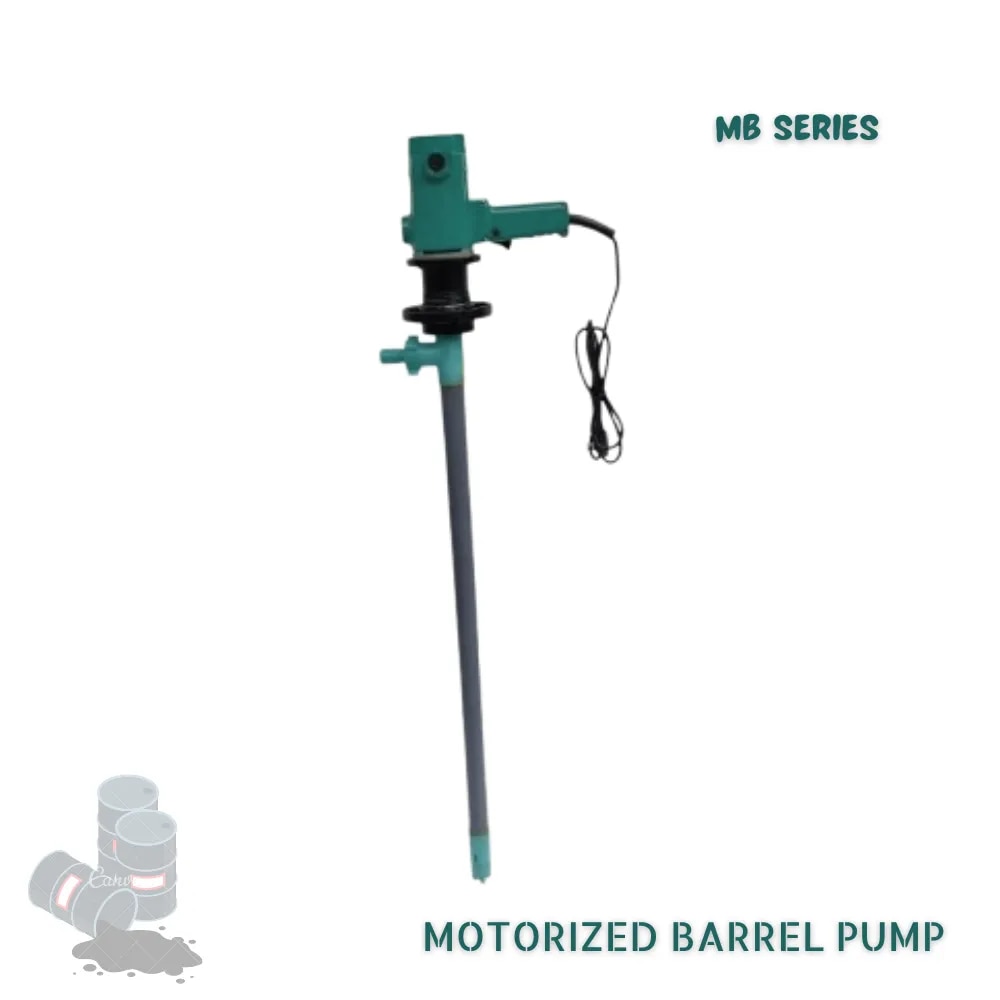
Motorized Barrel Pump
Description
Motorized Barrel Pump – Denwell Fluid Controls
Denwell Fluid Controls offers industrial pumping solutions including barrel pumps for liquid transfer applications. A Motorized Barrel Pump is designed for transferring liquids directly from drums, barrels, tanks, and other containers using an electrically driven pumping mechanism.
The motorized configuration provides powered liquid transfer without requiring manual pumping. It can be considered for industrial applications where repeated or controlled transfer of compatible liquids is required.
The exact pump construction, tube length, motor power, flow rate, discharge pressure, wetted material, and seal arrangement should be selected according to the liquid characteristics and application requirements.
Motorized Barrel Pump
A Motorized Barrel Pump is a compact liquid-transfer solution designed to pump liquids from barrels and drums into process lines, storage tanks, containers, or other receiving systems.
The pump is driven by an electric motor, providing consistent powered operation for liquid transfer. Depending on the selected construction, motorized barrel pumps can be used for compatible industrial liquids across chemical, manufacturing, processing, and utility applications.
For chemical or corrosive liquids, material compatibility between the liquid and wetted pump components is an important consideration. Parameters such as viscosity, temperature, specific gravity, required flow, and discharge head should also be evaluated before selecting the pump.
Key Features
Motor-driven barrel pumping system
Designed for liquid transfer from drums and barrels
Compact and practical construction
Powered operation for repeated liquid transfer
Suitable for industrial liquid-handling applications
Easy integration with suitable storage and process systems
Available with application-specific wetted materials
Suitable for transferring compatible liquids
Useful for drum-to-tank and container-to-process transfer
Application-based pump selection
Applications
Motorized Barrel Pumps can be considered for:
Chemical liquid transfer
Drum-to-tank transfer
Barrel-to-container transfer
Industrial liquid handling
Process-liquid transfer
Solvent transfer where compatible
Chemical processing
Manufacturing plants
Water and utility-liquid transfer
Storage tank filling
Batch-processing applications
The actual suitability depends on the liquid, viscosity, temperature, chemical compatibility, required flow rate, head, and operating conditions.
Q&A – Motorized Barrel Pump
1. What is a Motorized Barrel Pump?
A Motorized Barrel Pump is an electrically powered pump designed to transfer liquids from barrels, drums, containers, and similar storage vessels.
2. How does a Motorized Barrel Pump work?
The pump uses an electric motor to drive the pumping mechanism. The pump tube is positioned inside the barrel or drum, allowing the liquid to be transferred through the discharge connection to another container, tank, or process line.
3. What is a Motorized Barrel Pump used for?
It is primarily used for transferring liquids from drums and barrels. Typical applications include chemical transfer, process-liquid handling, storage-tank filling, and industrial fluid transfer.
4. What is the advantage of using a motorized barrel pump?
Motorized operation eliminates the need for manual pumping and provides powered liquid transfer. It can be useful where liquids need to be transferred repeatedly or where manual handling is inconvenient.
5. Can a Motorized Barrel Pump be used for chemicals?
Yes, a suitable motorized barrel pump can be selected for compatible chemicals. The pump material, seals, gaskets, temperature rating, and other wetted components must be compatible with the specific chemical.
6. Can it transfer corrosive liquids?
It can be considered for compatible corrosive liquids when the pump construction is selected appropriately. Chemical concentration, temperature, and material compatibility should be evaluated before selection.
7. Can a Motorized Barrel Pump handle viscous liquids?
The suitability depends on the viscosity and the specific pump design. Higher-viscosity liquids may require a pump configuration specifically designed for the required viscosity and flow conditions.
8. Where can a Motorized Barrel Pump be installed?
It is generally used directly with drums, barrels, tanks, and other suitable containers. The pump tube is inserted into the liquid container and connected to the appropriate discharge arrangement.
9. What factors should be considered when selecting a Motorized Barrel Pump?
Important parameters include:
Liquid type
Viscosity
Temperature
Specific gravity
Required flow rate
Discharge head
Barrel or drum dimensions
Wetted material compatibility
Motor power
Operating frequency
Required duty cycle
10. Can a Motorized Barrel Pump be used for drum-to-tank transfer?
Yes. Drum-to-tank transfer is one of the common applications for powered barrel pumping systems, provided the pump is correctly selected for the liquid and required transfer conditions.